If you’re in the food packaging game, chances are you’ve crossed paths with paper lunch box forming machines. I’ve been supplying these bad boys for 8 years now, and let me tell you—they’re workhorses, but like any machine that runs 12 hours a day, they throw their fair share of curveballs. Most of the problems aren’t even that complicated, but if you’ve never dealt with them, they can bring your whole production line to a grinding halt. Today I’m breaking down the most common headaches I see, plus the quick fixes that actually work, not the generic “call a technician” fluff. Paper Lunch Box Forming Machine

First off, let’s get one thing straight: paper lunch box forming machines are finicky about the raw material. If you’re loading in cheap, flimsy paper stock that’s not cut or coated right, you’re setting yourself up for issues before you even hit the start button. That’s a tip I give every new client within the first 10 minutes of them signing an order. But enough setup—let’s dive into the problems.
The number one issue I get calls about every single week: uneven box sides or boxes that won’t hold their shape. You crank out a batch, they look all lopsided, and by the time you stack them, half collapse. 9 times out of 10, this isn’t a broken part—it’s a tension problem. The machine’s roller systems that feed the paper are either too tight in some spots and too loose in others, or there’s a kink in the paper roll that no one noticed when loading. Last month I had a customer who swore their machine was busted, turned out they’d loaded a new roll with the cardboard core still partially in, so the paper was unevenly fed. The fix here is simple: every 2 hours, stop production, do a quick check of the feed rollers. Wipe them down with a lint-free cloth (static builds up, especially in dry weather, and makes paper stick weird), adjust the tension knobs until you feel consistent resistance when you pull a foot of paper through, and make sure there’s no crease or tear running along the roll. If you’re using coated paper (the kind that’s grease-resistant for takeout), check that the coating is evenly applied too—thicker spots on the coating can make the forming dies grip unevenly. I’ve had clients skip this check and burn 3 hours of production just re-forming lopsided boxes that got stuck on the conveyor.
Next up: boxes sticking to the forming dies. This is the worst because it stops the line cold every 5 minutes, and you end up with a mess of paper stuck to metal parts. Why does this happen? Mostly two things: leftover adhesive or residue on the dies, or heat that’s too high. Wait—heat? Yeah, a lot of people crank up the temperature to make the paper fold easier, but if it’s over the optimal range (usually 150-175°C for most stock), the coating on the paper melts and sticks like glue. A lot of my new clients forget that the optimal temp is tied directly to the paper grade they’re using. If you switched from a lightweight stock to a thicker one last week, you can’t just keep the temp the same—you might need to bump it up 10°C, but not more. For the residue problem: every shift, before you start, wipe the forming dies with a non-abrasive cleaner (no steel wool, that scratches the metal and makes sticking worse) and a tiny bit of silicone spray, not too much. Silicone creates a non-stick layer that doesn’t transfer to the boxes. I had a bakery client who tried using dish soap to clean dies, and guess what? The soap left a residue that made every box stick for a full week. Don’t do that. If sticking happens mid-run, pause the machine, blast a little compressed air at the die, and gently pry the paper off with a plastic spatula—metal will scratch, trust me.
Third common issue: misaligned box flaps. When you fold the side flaps or the top flaps, they don’t line up, so when you seal the box, it’s crooked and can’t hold food. This is usually a simple calibration issue, not a broken sensor. A lot of people don’t know that the forming dies’ guides adjust over time—vibration from the machine running 10+ hours a day will loosen them up. The fix here is to run a test piece every 500 boxes, not every 1000 like some clients do. Grab a freshly formed box, lay it flat on a table, check if the side flaps are the same length. If one is longer, loosen the guide screws on that side, slide it over 1mm or 2mm, tighten, and test again. Don’t over-adjust—small tweaks go a long way. I had a client last year who was 10mm off on the guides, so every box flap was impossible to fold, and they were blaming the machine’s forming mechanism. Took me 10 minutes to adjust the guides, and they were back to full production. Also, watch out for the pressure pads that hold the paper in place while folding—if those are worn down, they don’t keep the paper tight, so flaps shift. If you notice they’re smooth instead of slightly grippy, replace them—they’re cheap, and way easier than troubleshooting misaligned flaps for days.
Now, the issues that come with the machine’s moving parts, not just material or settings. Jamming is obvious, but not all jams are the same. The most annoying jam is a hidden one—paper gets wedged in the feed track, and you don’t notice until you’ve run 100 boxes with half the paper torn. Why does that happen? Most often, the machine’s in-feed rollers are dirty, or there’s a tiny piece of leftover paper from the last run stuck in the track. I tell all my clients to do a full deep clean at the end of every shift: pull out all the rollers, wipe them down with rubbing alcohol, blow out the feed track with compressed air to get rid of paper dust and tiny scraps. Paper dust builds up over time, mixes with a little bit of lubrication from the machine, and turns into a sticky gunk that traps paper. I’ve had a client go 2 weeks without deep cleaning, and they had a jam that took 2 hours to fix because paper was wedged so far back in the track. Quick jam fix: if you see a tear, turn the machine off immediately—don’t keep running it to “work it out,” that just tears more paper and damages the rollers. Unplug it if you have to to be safe, then carefully pull the paper out from the end, not the feed side. Pulling from the feed side will only jam it further.
Last common problem: inconsistent seam sealing. The edges of the box that get folded and glued don’t stick, so when you put hot food in, the box leaks. This is a mix of adhesive and temperature, but also the pressure from the sealing rollers. First, make sure you’re using the right adhesive for paper lunch boxes—hot melt adhesive is standard, but if you’re using a cheap adhesive that’s not formulated for coated paper, it won’t bond. I always recommend grade A hot melt for my clients, not the generic stuff from the hardware store. Then, check the sealing roller pressure: if they’re too loose, the adhesive doesn’t get pressed into the paper; too tight, you crumple the edge. The sweet spot is when you can press down on the sealed seam with your thumb and it doesn’t pull apart, but you don’t see adhesive oozing out the sides. Also, if the sealing rollers are worn down, they won’t apply even pressure—replace them every 6 months, or sooner if you see smooth spots from use. I had a takeout chain client that was going through 20 boxes of lost product a week because of bad seams; we adjusted the pressure, swapped out the rollers, and cut that waste by 90% in a week.
A lot of people think these problems are the machine’s fault, but 90% of the time, they’re user error or lack of regular small maintenance. You don’t need a $1000 technician every time—most of these fixes take 15 minutes, if that. The key is small, consistent checks, not waiting for a big problem to pop up. I’ve had clients who run their machines 24/7 with zero downtime because they do a 10-minute check every shift, and others who call me crying because their line is down for a day because they skipped a simple adjustment.
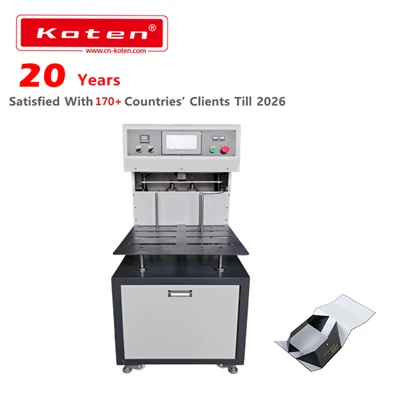
If you’re dealing with any of these issues, or you’re looking to upgrade your machine to cut down on downtime and waste, don’t mess around with guesswork. I’ve worked with small bakery owners and huge national food brands, so I know how important it is to keep production moving without overspending on repairs or wasted material. Hit me up to talk through your specific setup, or if you’re in the market for a new machine that’s built to handle the daily grind, not just perfect test runs. We can go over specs, adjust settings for your exact paper stock, and make sure you don’t end up pulling your hair over lopsided boxes or stuck dies. Trust me, I’ve seen it all, and I can save you a lot of headaches.
Book Making Solutions References
- Paper Packaging Machinery Operation & Maintenance Guide. International Food Packaging Association, 2022.
- Best Practices for Forming and Sealing Paper Food Containers. Journal of Packaging Technology and Science, vol. 35, no. 4, 2021, pp. 187-202.
- Troubleshooting Common Paper Forming Machine Issues. Global Packaging Solutions, 2023.
Ruian Koten Machinery Co., Ltd.
Ruian Koten Machinery Co., Ltd. is one of the most professional paper lunch box forming machine manufacturers and suppliers in China, featured by quality products and good price. Please rest assured to buy CE approved paper lunch box forming machine made in China from our factory. Welcome to contact us for quotation.
Address: Room 2201, No. 2 Building, Rui Xiang Yi Hao, Ruixiang New Area, Ruian City, Wenzhou, Zhejiang, China.
E-mail: manager@cn-koten.com
WebSite: https://www.kotenmachinery.com/
