If you’ve ever ordered a custom turned part for a medical device, a prototype automotive component, or even a small-batch aerospace fitting, you might not have stopped to ask how that seemingly simple, precision-machined piece makes it from a design sketch to your doorstep. At our custom turned parts shop, we hear this question all the time—from first-time clients who only know they need a part that fits, to experienced engineers who’ve spent years navigating the gap between CAD files and physical components. The short answer? CNC (Computer Numerical Control) turning machines are the unsung workhorses behind nearly every high-quality custom turned part, and their role goes far beyond just “cutting metal.” Let’s break down why these machines are non-negotiable for anyone needing parts that are accurate, repeatable, and tailored to exact specs—no one-size-fits-all shortcuts allowed. Custom Turned Parts
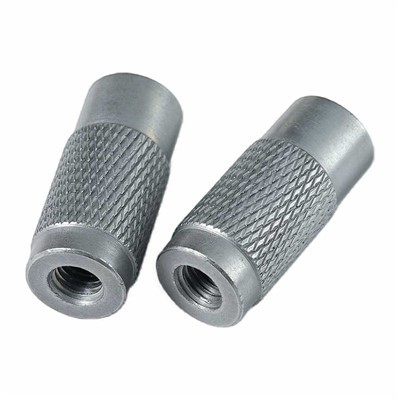
First, let’s ground this in what custom turned parts actually are, because too many people group them in with generic machined parts and miss the unique value of turning. Unlike milling, which removes material from a stationary part with a spinning cutting tool, turning revolves the workpiece around a central axis while a single-point cutting tool moves linearly to remove material. This process is ideal for making parts with symmetrical shapes—pins, bushings, shafts, adapters, valve bodies, and even small aerospace fasteners—that need uniform diameters along their length, smooth surfaces, and tight dimensional tolerances. The “custom” piece here is what makes it tricky: a off-the-shelf shaft won’t work if your design requires a 0.002-inch tolerance on the outer diameter, a keyway cut at a specific angle, or a thread pitch that only exists for your unique application. That’s where CNC turning steps in to eliminate the flaws of manual turning, which was the standard for custom parts before the 1970s.
Manual turning relied on a machinist’s skill to turn a handwheel that moved the cutting tool along X and Z axes, adjust the spindle speed in real time, and judge when the part was to spec. For small, one-off projects, manual turning works—but it’s error-prone. A new machinist might miss a tolerance, an experienced one might get fatigued on a 10-part batch, and there’s no way to replicate a perfectly identical part 100 times without writing down every single movement. For our shop, that’s a non-starter. We work with clients who need parts that fit into life-saving medical devices, where a 0.005-inch misalignment can cause a pump to fail; or automotive racing components, where a slightly off balance part can lead to catastrophic engine damage; or renewable energy parts, where outdoor exposure requires precise surface finishes to resist corrosion. Manual turning can’t deliver that level of consistency, and that’s exactly why CNC machines have become the backbone of custom turned parts manufacturing.
Now, let’s get specific about the role of CNC turning machines here, because it’s not just about automation—it’s about precision, flexibility, and scalability. First, precision. CNC machines run off G-code, a set of pre-programmed instructions that tell the machine exactly how fast to spin the workpiece, where to move the cutting tool, how deep to cut, and when to pause. That code is generated directly from a client’s CAD (Computer-Aided Design) file, so there’s no human interpretation of specs at the first step. For example, if a client designs a custom bushing with an inner diameter (ID) of 0.375 inches ±0.0005 inches, the G-code will be written to cut that ID to exactly 0.375 inches, with no room for a machinist’s judgment call. The machine’s linear and spindle movement is accurate to 0.0001 inches in many cases—way finer than the human eye or hand can manage. That precision doesn’t just make the part work; it reduces waste, too. In manual turning, if a machinist cuts a part slightly too small, it’s often scrap. With CNC, we can run a test cut on a sample workpiece, measure it with a coordinate measuring machine (CMM) to confirm alignment, and adjust the G-code once before running the full batch—so scrap rates drop to less than 1% for most projects, even for complex custom parts.
Next, flexibility. One of the biggest myths about CNC machines is that they only do high-volume parts. At our shop, we regularly run orders of 1 part, 50 parts, and 5,000 parts using CNC turning, because the same machine can adapt to whatever we need. For a one-off prototype, we input the CAD file, program the G-code in an hour, and run the part the same day—no need to build custom tooling that would be wasted after one use. For a 5,000-part order of identical valve stems, we can set the machine to run 24/7 with minimal supervision, because the G-code ensures every part is exactly the same. That flexibility is game-changing for custom turned parts, because most custom projects fall somewhere between prototype and high volume. A medical device startup might need 10 prototypes to test, then 500 production parts to launch—CNC turning handles both without retooling or sacrificing quality. Compare that to manual turning, where setting up for a new part can take hours, and you can’t reliably run more than 20 parts without deviating from the first, and it’s clear why CNC is the right tool for custom work.
Wait, but what about parts that need more than basic turning? A lot of custom turned parts aren’t just straight cylinders. They have features like cross holes, threads, chamfers, groves, or even complex shapes like cones or spherical ends that require secondary operations. Modern CNC turning machines have live tooling—small cutting tools mounted on the turret of the lathe, not just the main cutting tool. That means instead of moving the part to a separate milling machine to drill a cross hole, we can do it all on the same CNC lathe in one setup. That cuts down on setup time, reduces the risk of error from moving the part between machines (called fixturing error), and delivers tighter tolerances. For example, if a client needs a custom pin for a robotics arm that has a threaded end on one side, a cross hole in the middle, and a spherical tip on the other, a manual turner would have to set up the part three times: once to turn the pin, once to drill the cross hole, once to mill the sphere. With a CNC lathe with live tooling, we do it all in one setup, and the total tolerance across all features is way tighter. That’s a huge value add for our clients, because it means fewer parts come back as misaligned or mis-cut, and the lead time is shorter.
Another key role of CNC turning machines is material versatility. Custom turned parts are made from a huge range of materials, depending on the application: stainless steel for medical implants, aluminum for aerospace brackets, brass for electrical connectors, titanium for racing components, even plastics like PEEK for food or medical use. Each material has different properties—some are soft and gummy, some are hard and abrasive, some have high melting points. CNC machines can be programmed to adjust spindle speed, feed rate, and cutting tool type for each material automatically, but even for custom jobs, we can tweak the G-code to optimize for the material. For example, machining titanium requires slower spindle speeds and sharper cutting tools to avoid work hardening, while machining brass can be done at higher speeds for faster material removal. Manual turning would require a machinist to adjust these settings by hand for every batch, which can lead to inconsistent part quality or tool breakage. CNC turning eliminates that, so we can work with almost any material our clients need, without sacrificing quality or speed.
Now, let’s talk about the real-world impact of this. Last year, we worked with a startup developing a portable insulin pump that required a custom turned part: a small, stainless steel valve body that regulates the flow of insulin. The specs were strict: outer diameter of 0.25 inches ±0.001 inches, inner diameter of 0.125 inches ±0.0005 inches, a precision thread for the connection to the pump’s reservoir, and a smooth surface finish to avoid catching on the patient’s skin. The prototype they had made with manual turning had a surface finish that was too rough, and the thread tolerance was off by 0.002 inches, which would have caused leaks in the final product. We used a CNC turning lathe with live tooling to produce the part in one setup, ran a sample batch of 10, tested them with a CMM to confirm all tolerances, and delivered 500 production parts in 10 days. The client didn’t have to retool, and the parts passed all their leak and durability tests on the first try. That’s the kind of problem-solving CNC turning delivers for custom parts— it’s not just about cutting to a drawing; it’s about making a part that works in the real world.
But it’s not all about the machine. The role of CNC machines is amplified by the people who program, set up, and operate them. At our shop, we have machinists who aren’t just running machines—they’re translating client needs into G-code, troubleshooting when a part isn’t cutting right, and advising clients on design tweaks that can make a part easier and cheaper to machine without sacrificing performance. For example, if a client designs a custom turned part with a 0.1-inch long, 0.05-inch wide keyway, a good machinist might suggest a slightly wider keyway or a chamfer on the end to reduce tool wear, which means fewer broken tools, less scrap, and a lower cost for the client. That collaboration would be harder with manual turning, because the machinist is focused on operating the machine, not optimizing the part.
Of course, CNC turning isn’t perfect. It requires upfront programming time, which is why very small one-off parts can sometimes be more expensive than manual turning. But for any custom part that needs tight tolerances, consistent quality, or more than a few units, CNC is the clear choice. It’s also worth noting that modern CNC machines are getting more flexible—many have automatic bar feeders that can load raw material without a machinist having to stop, so we can run lights-out for batches of 1,000 parts, which keeps lead times short and costs low.
If you’re reading this because you need a custom turned part, don’t make the mistake of assuming all machined parts are the same. The CNC turning machine is the bridge between your design on a screen and a part that meets your exact needs, whether you need one prototype or 10,000 production units. It’s the reason we can deliver parts that fit life-saving devices, high-performance cars, and renewable energy systems with the precision and consistency that manual turning can never match.
We work with clients across industries to turn their custom designs into functional, high-quality turned parts. If you have a project you’re ready to discuss, our team is here to help you navigate specs, material choices, and lead times to get the right part for your needs.
Aluminum Turned Parts References:
- Chemical Engineering Magazine. (2022). “CNC Machining: Precision for Modern Manufacturing.”
- Society of Manufacturing Engineers (SME). (2021). “Turning Technology for Custom Part Production.”
- Aerospace Industries Association (AIA). (2020). “Precision Machining Standards for Custom Components.”
- Journal of Manufacturing Processes. (2023). “Live Tooling in CNC Turning: Reducing Secondary Operations for Complex Parts.”
- Medical Device & Diagnostic Industry. (2022). “Machining Standards for Implantable Components: Tolerance and Surface Finish Requirements.”
Huizhou Quanyi Precision Hardware Products Co., Ltd.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
